Most teams spec silicone the way they pick a catalog part. They read “chemically inert,” assume it covers their fluid, and move on. The seal passes incoming inspection. It passes the first week in the field.
Then it swells. A gasket that measured to print comes back from a customer 12% oversize, soft, and weeping. Nobody changed the material. The fluid did exactly what the chemistry predicted — the spec just never accounted for it.
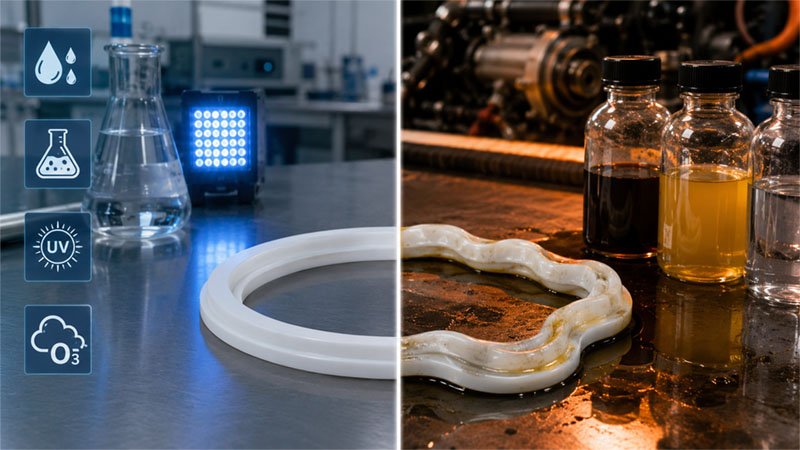
Silicone (VMQ) is inert toward water, alcohols, dilute acids and bases, ozone and UV because its Si–O backbone offers no easy reaction site. It is not universally resistant: nonpolar solvents and hot hydrocarbons swell it, strong oxidizers and concentrated acids degrade it, and standard grades have almost no oil or fuel resistance — which is exactly why fluorosilicone (FVMQ) exists. What follows is where that boundary actually sits, and how the resistance gets proven rather than assumed.
Executive Summary
- Inertness lives in the backbone, not the datasheet grade. The Si–O–Si chain resists oxidation, ozone and hydrolysis, but it does nothing to stop nonpolar solvents from diffusing in and swelling the network.
- “Compatible” means nothing without temperature, concentration, and exposure time. The same fluid can rate Recommended at 23°C intermittent and Not recommended at 100°C continuous immersion.
- Oil and fuel are the classic mis-spec. Standard VMQ swells badly in hydrocarbons; if there is oil, fuel, or aromatic solvent contact, the conversation moves to fluorosilicone, not a different silicone grade.
Why Silicone Is Inert: the Backbone, Not the Brand
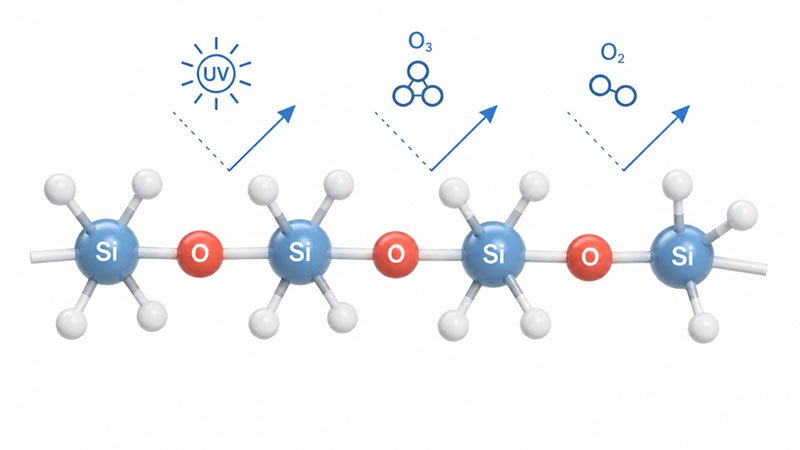
Silicone is a polysiloxane — an inorganic Si–O–Si backbone with methyl groups hanging off the silicon. Organic rubbers (NR, EPDM, NBR) are built on carbon–carbon chains. That difference is the whole story.
The Si–O bond is one of the strongest in commercial elastomers and has no double bonds in the main chain for ozone or oxygen to attack. So silicone shrugs off oxidation, UV, ozone, and weathering for 20-plus years outdoors where organic rubbers crack. Against water, alcohols, dilute aqueous acids and bases, it is genuinely stable.
But inertness toward reaction is not the same as resistance to absorption. Silicone is a relatively open, low-crosslink-density network. Small nonpolar molecules walk straight into it. The chemistry never reacts — the part just swells, softens, and loses sealing force. Teams conflate these two things constantly, and that is where most field failures start.
Where Silicone Holds
These are the environments where standard VMQ behaves as the “inert” reputation suggests:
- Cold and warm water, brine, and most aqueous salt solutions
- Methanol, ethanol, isopropyl alcohol, glycols, and glycerin
- Dilute mineral acids and dilute alkalis at ambient temperature
- Ozone, oxygen, and UV exposure — silicone is near best-in-class here
In these media the practical limits come from temperature and time, not chemical attack. Continuous hot water and low-pressure steam below ~100°C are tolerable for many grades; the failure mode there is slow hydrolysis and reversion, not swelling.
Where Silicone Gives: Swelling, Not Reaction
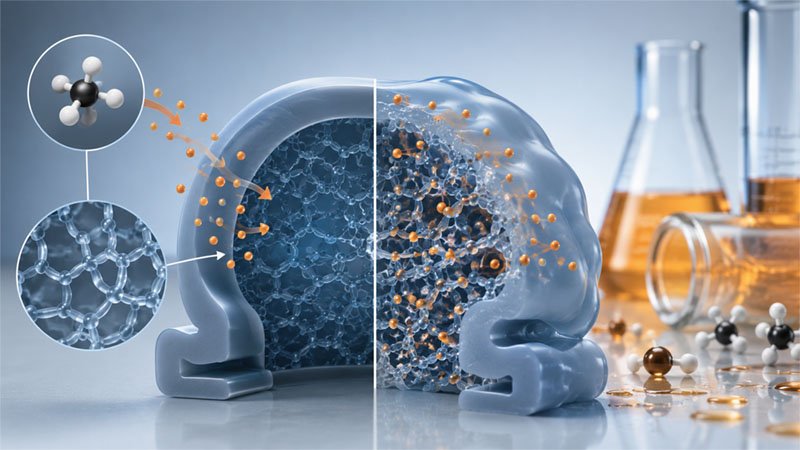
This is the half of the picture datasheets gloss over.
Aromatic and Chlorinated Solvents
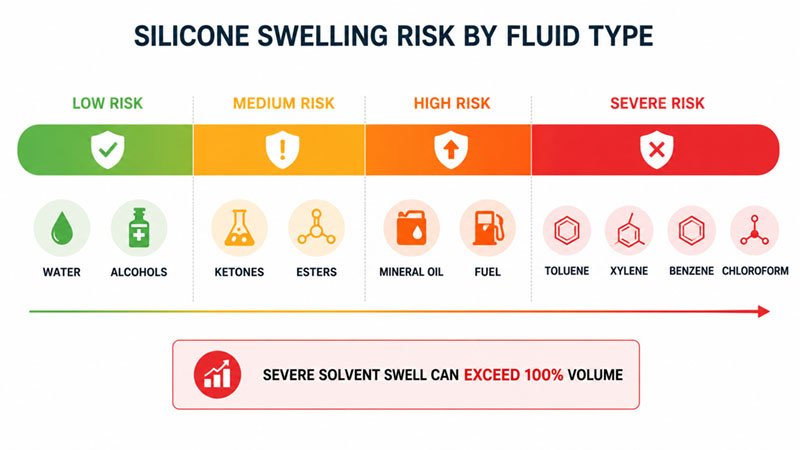
Toluene, xylene, benzene, carbon tetrachloride, and chloroform are the worst offenders. Standard silicone can swell 100–200% by volume in these — it absorbs the solvent like a sponge, balloons, and loses nearly all mechanical integrity. When the solvent flashes off, the part shrinks back, but rarely to its original dimensions or hardness. For sealing, that single swell/de-swell cycle is the end of the part.
Ketones and Esters
Acetone, MEK, and ethyl acetate cause moderate swell. Short, intermittent contact (a wipe-down, a cleaning step) is usually survivable. Continuous immersion is not.
Oils and Fuels — the One That Costs Money
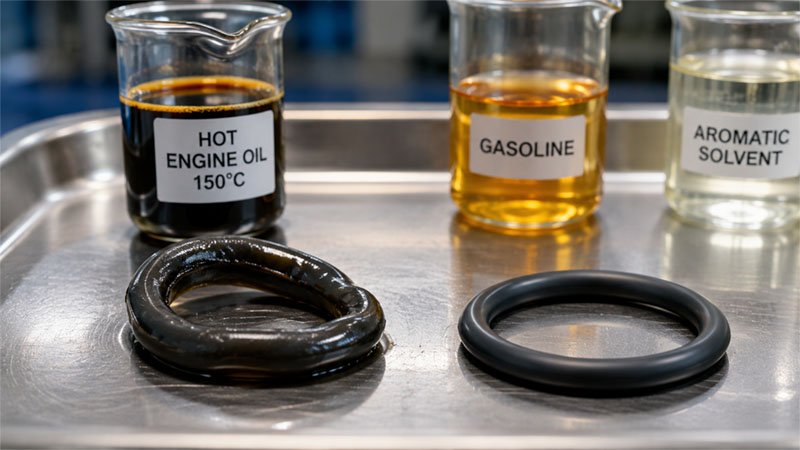
Standard VMQ has poor resistance to mineral oil, engine oil, gasoline, and diesel, especially hot. This is the most common and most expensive mis-spec I see, because the part looks fine until it sits in the fluid at temperature. If oil or fuel is in the system, the answer is fluorosilicone (FVMQ), which trades cost and some low-temperature flexibility for real hydrocarbon resistance. It is not a small price difference — confirm the fluid before quoting.
Where Silicone Actually Degrades
Swelling is reversible chemistry getting into the network. Degradation is the backbone breaking. The agents that do it:
- Concentrated sulfuric and nitric acid
- Hot concentrated alkalis (caustic attack of the Si–O bond)
- Strong oxidizers and superheated steam above ~120°C, which drive hydrolytic chain scission
Once the backbone is cut, there is no recovery and no de-swell. The part chalks, cracks, or turns gummy. For these media, silicone is the wrong base polymer — not a grade problem.
Does Silicone Absorb Odors and Tastes?
This comes up constantly on food and baby products, so it is worth being precise. Silicone does not chemically absorb odors. What it does is permeate. The same open network that lets gases pass through also lets odor and flavor molecules sorb into the surface and release slowly later. See silicone gas and vapor permeability for the mechanism.
There is a second, separate source: a fresh part with its own smell almost always means a peroxide-cured silicone that skipped or shortened its post-cure. Platinum-cured silicone has no reaction byproducts and is effectively odorless out of the mold. Peroxide-cured grades carry trace volatiles that need a proper post-cure (typically 200°C for ~4 hours) to drive off. If a customer reports odor on a food-contact part, check the cure system and post-cure record before blaming the material.
Silicone Chemical Compatibility Chart
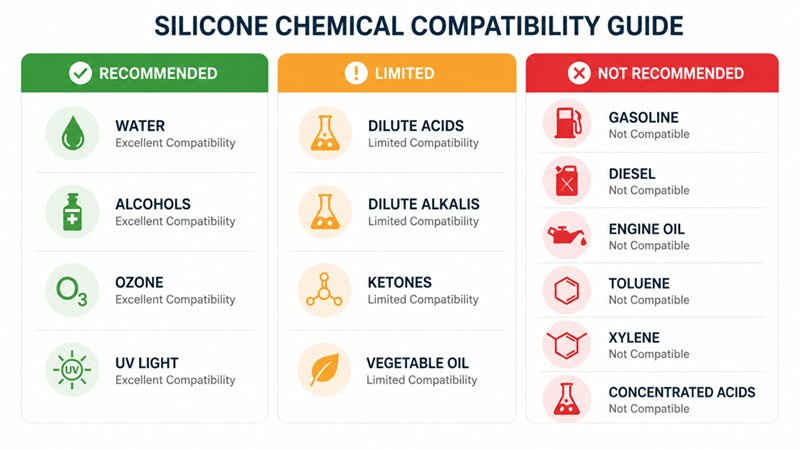
Ratings below are for general-purpose VMQ at ambient temperature, intermittent contact. R = Recommended (little to no effect), L = Limited (measurable swell or property change; conditional use), N = Not recommended (heavy swell or degradation). Treat this as a screening tool, not a sign-off — see the testing section for why.
| Medium | VMQ rating | Behavior |
|---|---|---|
| Water (cold) | R | Stable; primary limit is temperature |
| Hot water / steam ≤100°C | L | Slow hydrolysis on long continuous exposure |
| Superheated steam >120°C | N | Hydrolytic chain scission / reversion |
| Salt / brine, seawater | R | Inert |
| Dilute mineral acids (<10%) | L | Tolerated cold; avoid hot or concentrated |
| Concentrated sulfuric / nitric acid | N | Backbone degradation |
| Acetic acid (dilute) | L | Minor effect cold |
| Sodium hydroxide (dilute) | L | OK cold; hot caustic attacks Si–O |
| Concentrated / hot alkali | N | Caustic degradation |
| Ammonia solution | L | Mild effect |
| Methanol / ethanol / IPA | R | Negligible swell |
| Ethylene glycol | R | Inert |
| Glycerin | R | Inert |
| Acetone | L | Moderate swell; intermittent only |
| MEK / ethyl acetate | L | Moderate swell |
| Toluene / xylene / benzene | N | Severe swell (often >100% vol) |
| Carbon tetrachloride / chloroform | N | Severe swell |
| Mineral / engine oil (hot) | N | Use fluorosilicone instead |
| Gasoline / petrol | N | Heavy swell; FVMQ required |
| Diesel fuel | N | Heavy swell; FVMQ required |
| Vegetable oil | L | Slow swell; acceptable for many food uses |
| Silicone oil | N | Like dissolves like — swells |
| Ozone | R | Near best-in-class |
| Hydrogen peroxide (dilute) | L | OK dilute; avoid concentrated |
| Sodium hypochlorite (bleach) | L | Tolerated dilute; surface attack when concentrated |
How Chemical Resistance Is Actually Proven
A letter on a chart is a starting hypothesis. The number that matters is volume swell measured under defined conditions. Two standards govern this:
- ASTM D471 — Effect of Liquids on rubber. Measures change in mass, volume, hardness, tensile strength and elongation after immersion in a specified fluid, at a specified temperature, for a specified time (e.g., 70 hours at 23°C, 100°C, or 150°C).
- ISO 1817 — the equivalent international method for the effect of liquids on vulcanized rubber.
The output is the honest answer: a part might show +3% volume in a fluid at 23°C and +40% in the same fluid at 100°C. Same material, same chemical, opposite verdict. This is the core of Mode 3 thinking — the risk is not a bad material, it is reading a compatibility rating without its conditions attached.
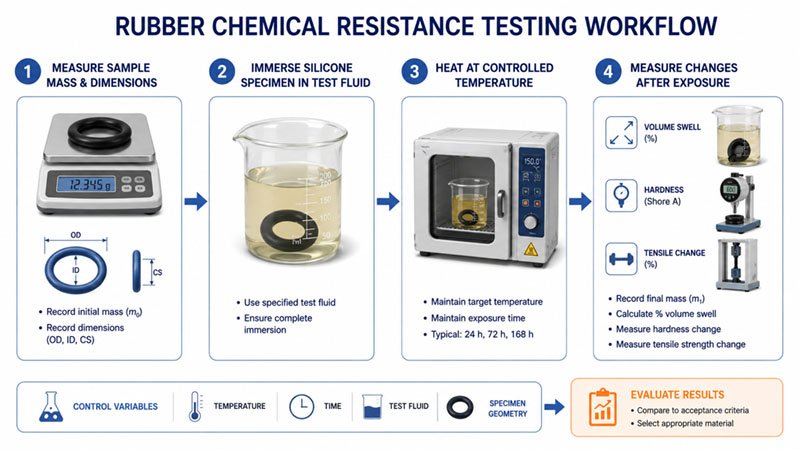
A usable resistance spec needs four things on it: the exact fluid (and concentration), temperature, duration, and whether contact is intermittent or continuous immersion. Without those, “silicone is compatible” is not a specification — it is an opinion.
Why Teams Underestimate This
The failure is almost never incompetence. It is that silicone’s headline reputation — inert, food-safe, weatherproof — is true in the conditions people first encounter it, so it gets generalized. A designer who saw silicone survive sun, water, and cleaning chemicals assumes it will survive the gearbox oil too.
The second trap is the test gap. Bench checks happen at room temperature with short exposure, which is exactly where swelling is mildest. The fluid contact in the real application is hotter and continuous, and that is where the volume change goes nonlinear. The part passes validation and fails in service, and the chemistry was never the surprise — the conditions were.
The third is treating cure chemistry as irrelevant to chemical behavior. Cure system drives odor, extractables, and food/medical compliance as much as the base polymer does. A peroxide-cured part and a platinum-cured part can read identically on a generic compatibility chart and behave differently in a migration test.
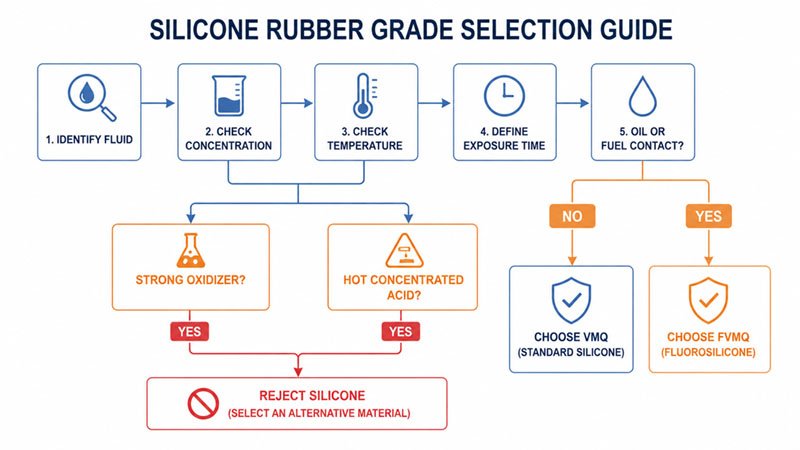
What I Need Before Confirming a Grade
This is where the conversation has to get specific. Before I commit a grade and a cure system, send:
- The exact chemical and its concentration (not “solvent” or “oil”)
- Operating and peak temperature at the contact point
- Exposure pattern: intermittent wipe/splash vs continuous immersion, and total service life
- Compliance target if any (FDA 21 CFR 177.2600, LFGB, USP Class VI)
- Whether low-temperature flexibility matters, since fluorosilicone gives up some cold performance for its oil resistance
With those five inputs I can tell you whether standard VMQ holds, whether it needs fluorosilicone, or whether silicone is the wrong base polymer for the fluid. Without them, any rating I give you is a guess dressed up as a spec.