We quote both silicone and TPE every week, and most buyers arrive with the wrong question. They ask which material is “better.” That comparison has no answer. The real question in silicone vs TPE is which one survives your part’s temperature, compliance, and volume — and that answer is usually locked in before you ever send a drawing.
The trap is that generic “it depends” advice pushes the decision downstream, where it gets expensive. Choose TPE for a part that sees 160°C and you find out after the tool is cut. Choose silicone for a low-margin consumer accessory and the unit cost kills the program. Neither mistake shows up on day one.
Here is how we actually decide on the floor.
Executive Summary
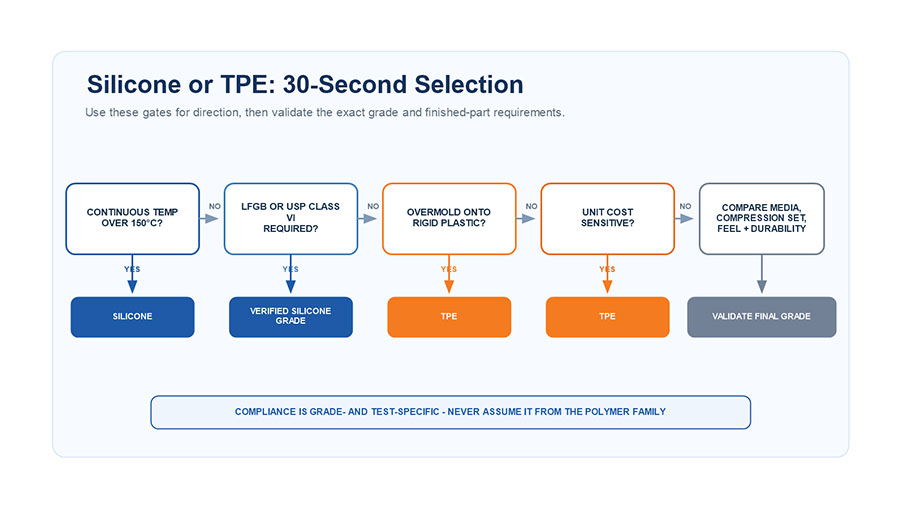
- Temperature and compliance decide silicone; cost and volume decide TPE. If continuous service passes ~150°C, or the part needs LFGB / USP Class VI / ISO 10993, the material is silicone before cost enters the conversation.
- TPE wins on unit economics and cycle time. It runs on standard thermoplastic injection, scrap can be reground, and cycles are seconds, not minutes.
- The irreversible cost is tooling. LSR silicone needs a heated, often cold-runner mold; switching materials later almost always means cutting a new tool.
Should You Choose Silicone or TPE? The 30-Second Answer
Choose silicone when the part must hold up to heat, repeated sterilization, or strict food/medical compliance. Choose TPE when unit cost, recyclability, and fast molding matter more than thermal limits.
| Decision driver | Points to silicone | Points to TPE |
|---|---|---|
| Continuous temp > 150°C | Yes | No |
| Food contact at LFGB level | Yes | Grade-dependent |
| Medical / USP Class VI / implant | Yes | No |
| Unit cost sensitive (>50k/yr) | No | Yes |
| Recyclable / regrind needed | No | Yes |
| Overmold onto PP / PC / ABS | Harder | Yes |
| Soft-touch, low-temp consumer part | Works | Yes (cheaper) |
Silicone vs TPE: Thermoset vs Thermoplastic Is the Real Decision
Everything traces back to one structural fact: silicone is a thermoset, TPE is a thermoplastic. Silicone cures irreversibly through cross-linking — once vulcanized it will not re-melt. TPE softens every time you heat it, which is exactly why it can be reground and re-injected.
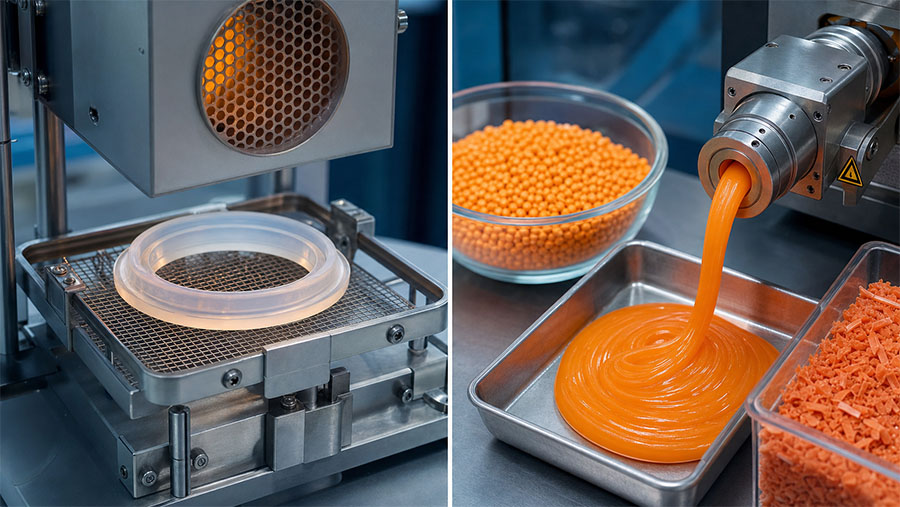
That single property drives heat resistance, recyclability, cycle time, and cost. Teams underestimate it because both materials feel similar in the hand — soft, rubbery, flexible. The behavior only diverges under heat and repetition, long after the sample gets approved.
How Hot Can Each Material Run?
Silicone holds a working range of roughly -40°C to 230°C, with high-temp grades taking short excursions to 250–300°C. Standard TPE tops out around 90–120°C for continuous use; harder TPV grades reach about 135°C.
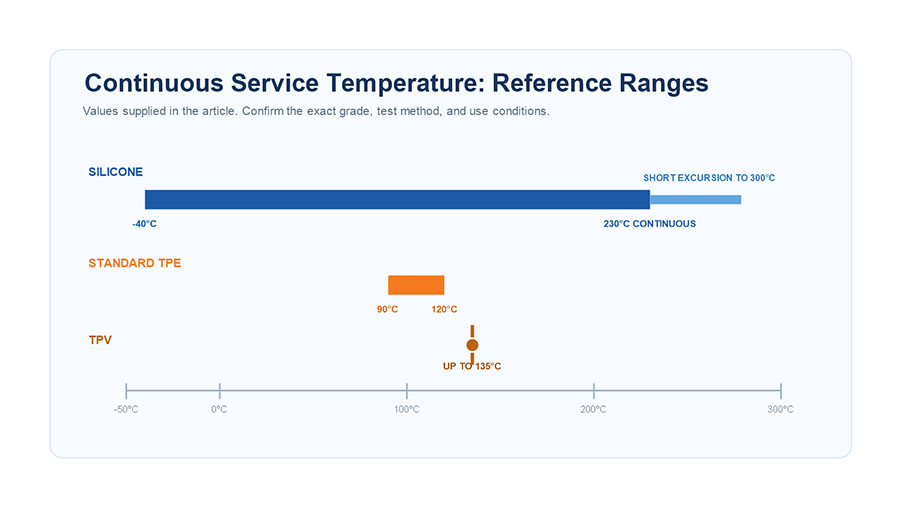
This is the cleanest dividing line we have. Anything near an engine bay, a steam sterilizer, or an oven is silicone by default. Where buyers get burned is intermittent heat: a part rated for 100°C ambient can still deform if it sees repeated 130°C wash cycles, because TPE creeps under load at temperatures well below its melt point.
Which Material Passes Your Compliance Requirement?
For food and medical, silicone clears the higher bars more easily. Platinum-cured silicone meets FDA 21 CFR 177.2600 and the stricter European LFGB, including overall migration testing. For medical, silicone reaches USP Class VI and ISO 10993 biocompatibility — which is why implants, menstrual cups, and IV components are silicone, not TPE. TPE has food and medical grades too, but qualification is grade-specific and plasticizer leaching is the recurring audit question.
The judgment gap: buyers assume “food grade” is a single pass/fail. It isn’t. LFGB-compliant silicone typically runs 20–30% more than a basic FDA grade, because it needs a cleaner base polymer and longer post-curing (often 200°C for 4 hours). If your spec just says “food safe,” you haven’t specified enough for us to quote.
When Does TPE Win on Cost and Lead Time?
TPE wins whenever thermal and compliance limits are not binding — and then it wins decisively. It molds on standard thermoplastic injection machines, scrap regrinds back into the process, and it does not carry the cure-driven cycle penalty that silicone does.
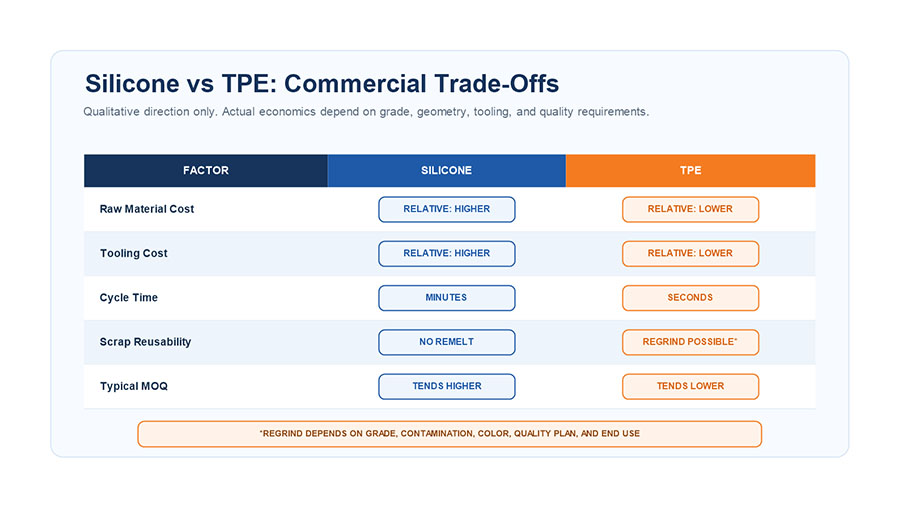
| Cost factor | Silicone (LSR / HTV) | TPE |
|---|---|---|
| Raw material | Higher; platinum grades priciest | Lower, commodity feedstock |
| Tooling | Heated mold, often cold-runner | Standard thermoplastic tool |
| Cycle time | 30s to several minutes (cure) | ~15–40s |
| Scrap / regrind | Not re-meltable; scrap is waste | Regrind reusable |
| Typical MOQ | Higher, to justify tooling | Lower, more flexible |
For a high-volume consumer part with no heat or medical constraint, the TPE program is usually cheaper on every line except tear strength and temperature.
Silicone Tooling and MOQ: The Irreversible Part
Silicone tooling is where the decision becomes permanent. LSR needs heated tooling and frequently a cold-runner system to avoid wasting cured material in the sprue; HTV compression tooling is simpler but slower and more labor-heavy, with wider tolerances and flash to trim. LSR holds tight tolerances (down to about ±0.02mm) and near-zero flash, but the mold is expensive and built for one material.
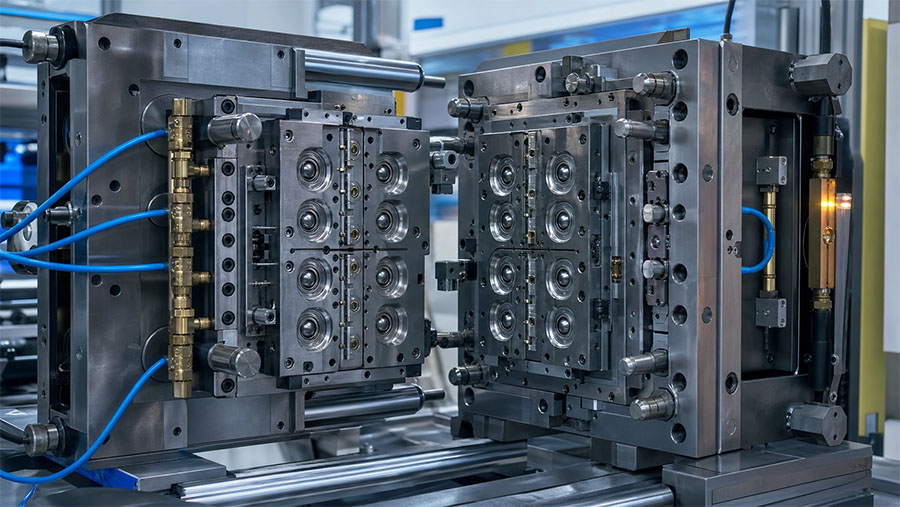
That is why we push buyers to settle temperature and compliance first. A tool cut for LSR does not transfer to a TPE program, and vice versa. “We’ll switch if it’s too expensive” is not a real option once steel is cut.
When Is TPE the Right Engineering Choice?
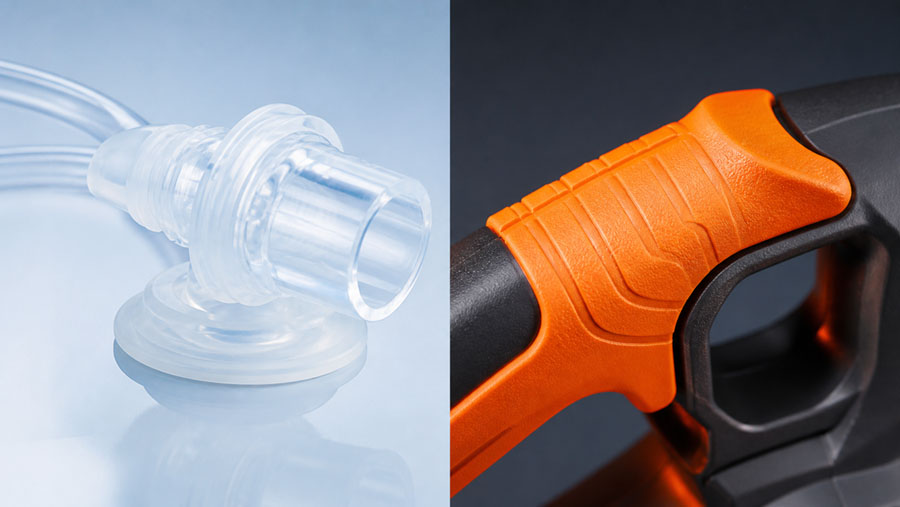
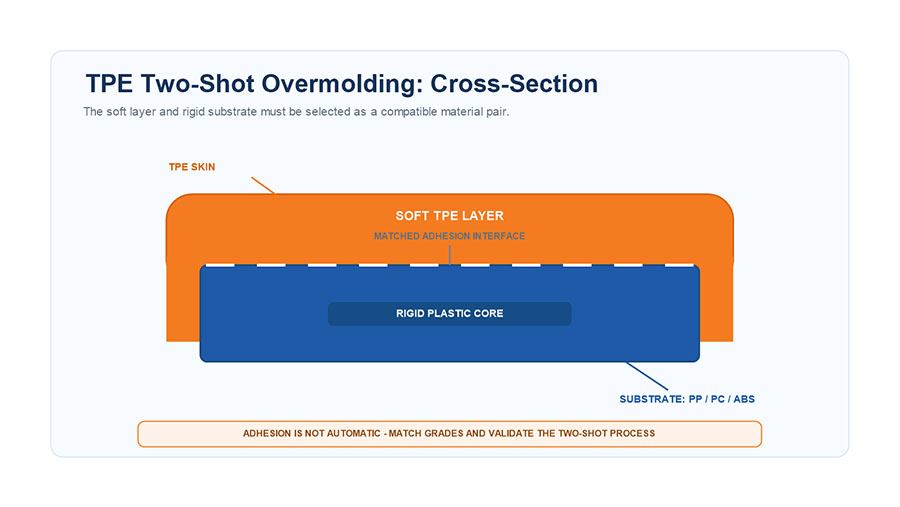
TPE is the correct choice — not a compromise — when the design is a soft layer over a rigid thermoplastic. TPE bonds to PP, PC, and ABS through standard two-shot overmolding: soft grips on tools, toothbrush handles, phone cases, cable jackets. Silicone-to-plastic bonding needs self-bonding LSR grades or primer plus a compatible substrate, which is more restrictive and more expensive.
So if your part overmolds onto a housing and never sees high heat or medical compliance, specifying silicone usually adds cost and tooling risk for no functional gain.
Common Misjudgments We Correct at Quote Stage
- “TPE is basically cheap silicone.” Different chemistry, different limits — not a downgrade of the same thing.
- “Food grade is one standard.” FDA 21 CFR 177.2600 and LFGB are different bars with different costs.
- “We’ll change materials if cost runs high.” Tooling rarely transfers; decide before cutting the mold.
- “Silicone is recyclable.” It is a thermoset and will not re-melt; recycling is niche and costly, unlike TPE regrind.
What Do We Need to Quote Your Part?
We can’t finalize silicone vs TPE from a shape alone. To lock the material and give firm pricing, send us: continuous and peak service temperature, required certification (FDA / LFGB / USP Class VI / RoHS), target Shore A hardness (our usable range is 10A–80A), annual volume, and whether the part overmolds onto a rigid substrate.
The two inputs that force a re-quote when they’re missing are temperature and compliance. Give us those, and the material choice is usually decided in one pass.