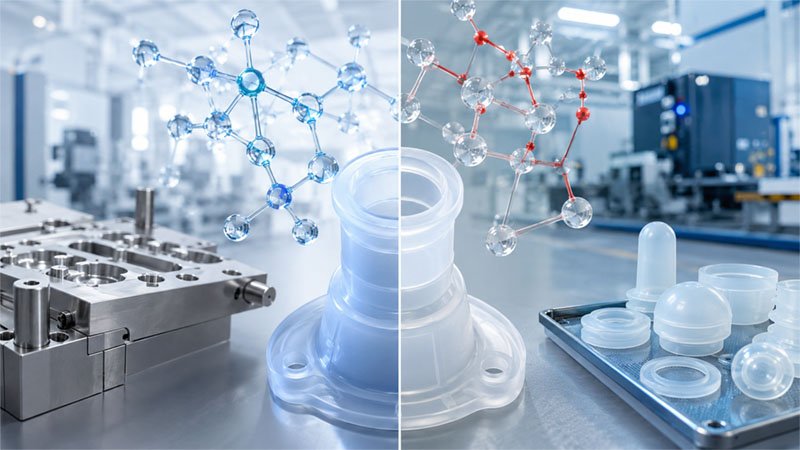
In silicone manufacturing, “curing” and “vulcanization” describe the same chemical event — cross-linking polysiloxane chains into a thermoset elastomer. The decision that actually matters is the cure chemistry: platinum (addition) vs peroxide (free-radical), because that choice controls food and medical compliance, odor, optical clarity, and unit cost.
Anyone searching this phrase expects two different processes. Most generic articles invent a fake split, which wastes RFQ cycles and leads to spec mistakes that surface only after the first 1,000 parts ship. Below is what the two words actually mean inside a silicone plant, and the cure-system choice you actually need to make.
Are Curing and Vulcanization Different?
No. In rubber chemistry, vulcanization was coined for Goodyear’s 1839 sulfur cross-linking of natural rubber. The term was later generalized to any thermoset cross-linking step. In silicone (polysiloxane) there is no sulfur involved at all — yet operators, datasheets, and ISO / ASTM documents still use both words interchangeably.
What the words refer to inside the factory:
- Cure time — how long the press, oven, or mold holds to lock the cross-links.
- Vulcanization temperature — the platen or oven set-point that triggers cross-linking.
- HTV — High-Temperature Vulcanization. Same material is also labeled “heat-cured silicone.”
- RTV — Room-Temperature Vulcanizing. Common for two-part sealants and mold-making compounds.
If a supplier insists the two words mean different processes, ask which cure system they are running. That is the question they should be answering.
What Actually Differs: Cure Chemistry
Three cure systems appear on silicone datasheets. The choice between them is locked at the material spec stage and is largely irreversible once tooling is cut.
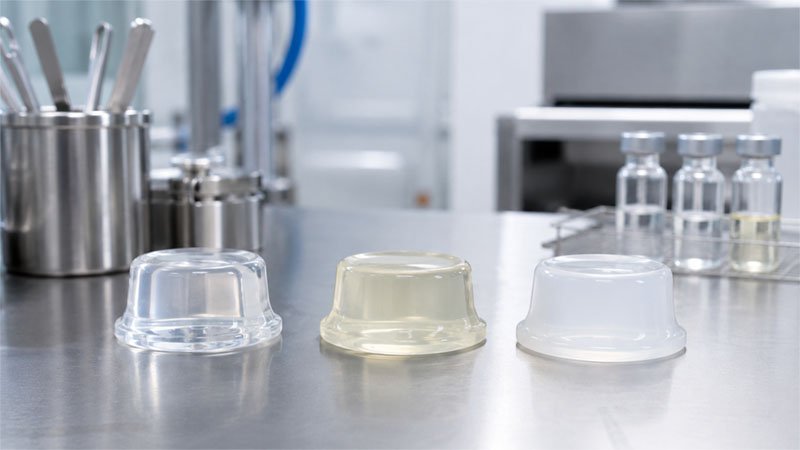
| Parameter | Platinum (Addition) | Peroxide (Free-Radical) | Condensation (Tin) |
|---|---|---|---|
| Catalyst | Pt complex (Karstedt-type) | DCBP / 2,4-DCBP / DBPH | Sn organotin (DBTDL etc.) |
| By-products | None | Aromatic acid residues — post-cure required | Methanol or acetic acid |
| Post-cure | Usually skipped or short | 200°C × 4 h typical, mandatory for food / medical | None (skin-cures in air) |
| Odor | None | Faint to noticeable without full post-cure | Acetic or alcoholic during cure |
| Optical clarity | Water-clear achievable | Slight yellow tint, drifts over time | Translucent at best |
| Food contact (LFGB / FDA 21 CFR 177.2600) | Default choice | Possible only after full post-cure | Not used |
| Medical (USP Class VI / ISO 10993-5,-10) | Standard | Rarely qualified | Not used |
| Typical material form | LSR + HCR | HCR (gum stock) | RTV-2 |
| Cost band (relative) | High | Low | Low to mid |
| Common failure mode | Pt poisoning (S, N, P, Sn) → tacky surface, undercured core | Skipped post-cure → odor, compression-set fail, LFGB migration fail | Slow skin-cure → bonding and dimensional issues |
Why Platinum Cure Is Easy to Misjudge
The catalyst is inexpensive on paper but easy to poison. Sulfur from neoprene gaskets, ammonia from line cleaners, or tin residues from condensation silicones running on the same machine will leave a tacky surface or an undercured core. Most “the part isn’t curing” complaints we receive from new clients trace back to contamination on the client’s side, not to the material itself. Pt-cure lines need dedicated tooling and clean handling — that operational cost is often missed when comparing the raw material price.
Why Peroxide Cure Looks Cheaper Than It Is
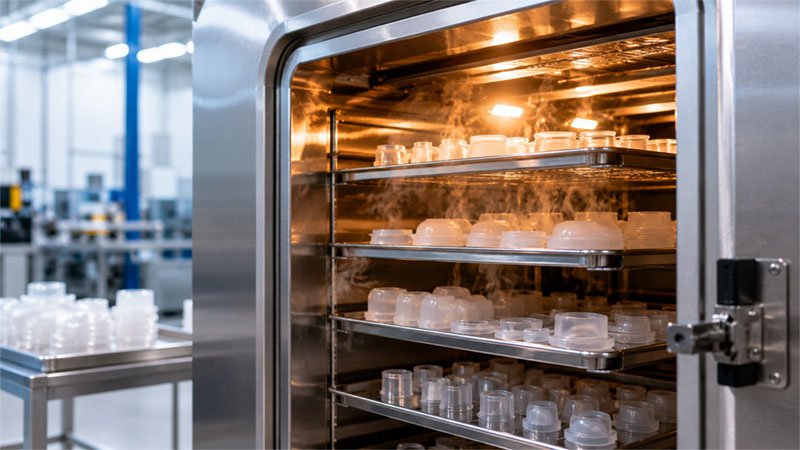
The press cycle is short, but the part is not finished when it demolds. Without post-curing at roughly 200°C for 4 hours, the part will fail compression set, smell on first use, and almost always fail LFGB overall migration. Teams skip the post-cure to save oven time and re-run the order three weeks later. The realised cost lands closer to platinum than the quote suggested.
HTV vs LSR vs RTV — The Axis Most Often Confused with “Curing”
Cure chemistry tells you what is cross-linking. Material form tells you how the material enters the press. The two axes are independent — most spec confusion comes from collapsing them into one word.
| Form | State at supply | Typical cure system | Process | Best fit |
|---|---|---|---|---|
| HCR / HTV | Solid gum | Peroxide or Pt | Compression / transfer molding | Mid-volume parts, larger cross-sections, Shore A 40–80 |
| LSR | Two-part liquid (A+B) | Pt only | Injection, cold-runner | High volume, tolerance ±0.02 mm, medical, infant feeding |
| RTV-2 | Two-part liquid | Condensation or Pt | Pour / cast | Mold-making, encapsulation, low-volume prototyping |
Where the Distinction Actually Costs Money
The spec-side mistakes we see most often, in order of frequency:
- “Food-grade silicone” without specifying Pt cure → factory defaults to peroxide HCR, post-cure gets shortened to hit lead time, LFGB §30 overall migration test fails on the audit sample.
- “Medical grade” written on a peroxide-cure datasheet → will not pass USP Class VI extractables; the part has to be re-quoted on LSR.
- Pt and condensation silicone on the same molding line → tin trace contamination poisons the next Pt batch; the line gets stopped for deep clean, and the Pt batch is scrapped.
These are not edge cases. They drive most of the re-mold and re-order traffic that hits our queue.
What to Lock on the RFQ Instead
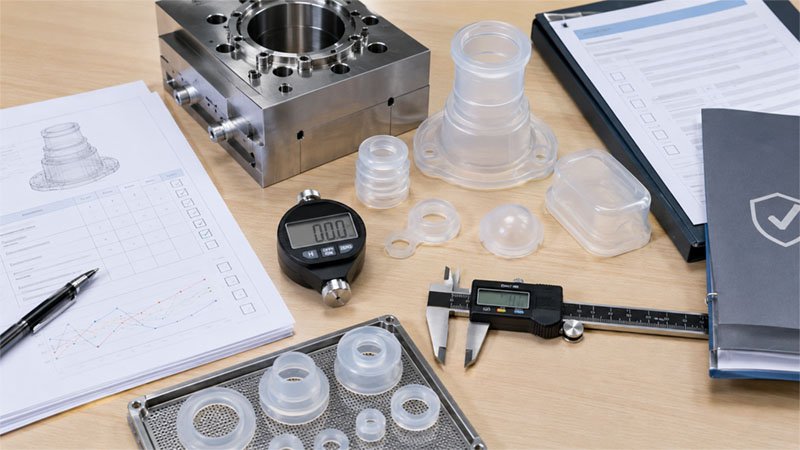
Replace “curing process” or “vulcanization method” with the four fields below. With these locked, a real quote comes back in a day. Without them, any “Pt vs peroxide” conversation on a supplier call is a stall.
- Cure chemistry: Platinum (addition) / Peroxide / Condensation
- Material form: HCR / LSR / RTV-2
- Shore A target ±5 points (e.g. 30A for infant nipple, 70A for kitchen tool handle)
- Compliance target: FDA 21 CFR 177.2600 / LFGB §30 + §31 / USP Class VI / ISO 10993-5,-10 / RoHS
- Post-cure conditions: required yes / no, and schedule (e.g. 200°C × 4 h)
- Optical / yellowing tolerance after 1,000 h UV exposure (matters for transparent parts only)
FAQ
Is vulcanization the same as curing in silicone?
Yes. The two words are used interchangeably on silicone datasheets and on the shop floor. The substantive question is which cure chemistry — Pt, peroxide, or condensation.
Why does silicone need post-curing if it is already “vulcanized”?
Peroxide cure leaves aromatic acid residues that fail compression set and food-contact migration tests. Post-curing at ~200°C for 4 hours volatilises those residues. Pt-cured silicone has no by-products and usually does not need post-cure for the same reasons.
Can a peroxide-cured silicone part pass FDA or LFGB?
It can pass FDA 21 CFR 177.2600 after full post-cure. LFGB §30 overall migration is tighter; passing is possible but the post-cure window must not be shortened to hit lead time.
Where the Conversation Should Go Next
Whether you call the step curing or vulcanization is a vocabulary question. The cost and compliance question is which cure chemistry, on which material form, with what post-cure schedule, against which compliance standard. Those four numbers, plus a Shore A target, are what move a quote from generic to real.