On the bench, Silicone Shore hardness looks like a single number you drop into a spec sheet. In production, it is one of the first things that locks your tooling, your demolding, and roughly half of how the part behaves once it ships.
Most drawings reach us saying “soft silicone” or “Shore 50.” Neither is a spec. “Soft” is a feeling. “50” with no scale (A? 00? D?) and no tolerance is a guess we are forced to interpret on your behalf. Choose the durometer for how the part has to seal, flex, or wear — not for how it should feel in your hand — and always confirm the scale (almost always Shore A) plus a tolerance (typically ±5 Shore A per ASTM D2240 hardness testing). Specify it wrong and you don’t lose a sample. You lose the mold, because a compound cut for one shrink rate rarely transfers cleanly to a softer or harder one.
Executive Summary
- Hardness is a trade-off dial, not a quality grade. Going harder buys structure and abrasion resistance and costs you tear strength, elongation, and sealing on uneven surfaces.
- Most silicone parts live between Shore A 20 and 70. Below that you are on the Shore 00 scale (gels, cushioning); Shore D is rare for rubber-state silicone and usually signals the wrong material choice.
- The expensive mistake is changing durometer after tooling. Different compounds shrink differently, so a late hardness change often means re-cutting steel, not swapping material.
Silicone Shore Hardness Scales: 00, A, and D
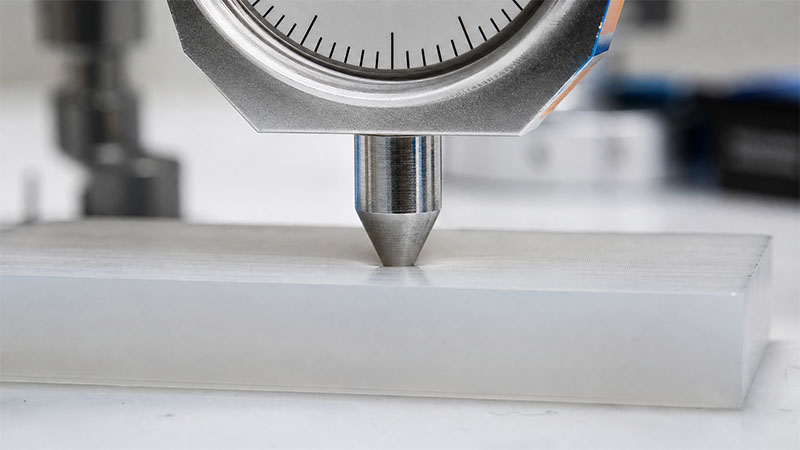
A durometer reading is meaningless without its scale. Three matter for silicone, and they overlap on purpose.
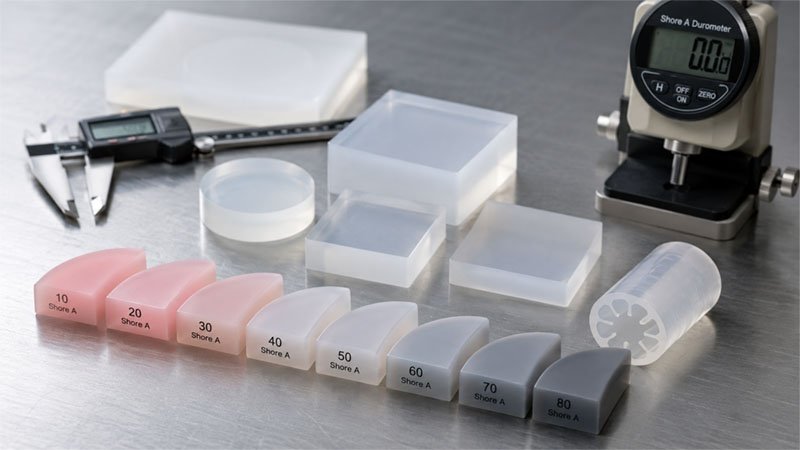
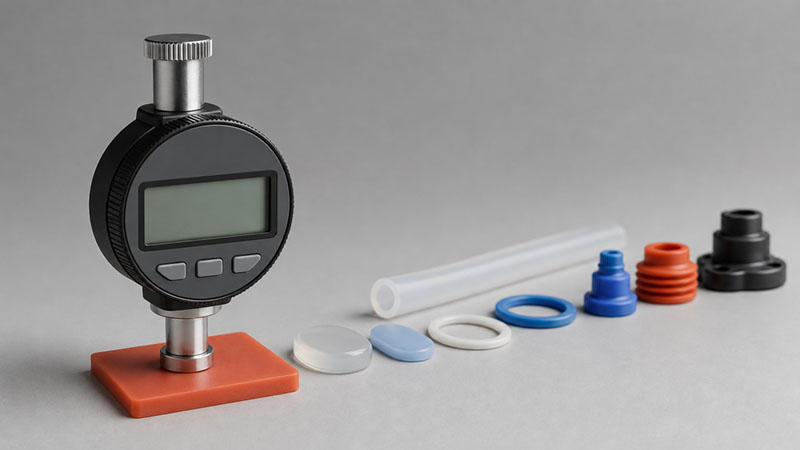
Shore A is the working range for nearly all molded silicone rubber. A durometer (per ASTM D2240, or ISO 7619 / ISO 48 for IRHD) presses a standardized indenter into a flat 6 mm specimen and reports resistance from 0 to 100. Shore 00 covers everything too soft for the A scale — gels, foams, fingertip-soft cushioning. Shore D only becomes relevant above the top of the A scale, in rigid-plastic territory; if your silicone part needs Shore D, you have usually picked the wrong polymer.
| Scale | Typical Range | What It Covers | Where It Belongs |
|---|---|---|---|
| Shore 00 | 00-20 to 00-50 | Gels, foams, very soft cushioning | Vibration pads, soft wearables, gel cushioning |
| Shore A | 10A to 80A | The working range for almost all molded silicone rubber | Seals, gaskets, tubing, keypads, baby and kitchen products |
| Shore D | Above 90 Shore A | Hard rubbers and rigid plastics | Rarely correct for silicone — usually a material error |
One more discipline most specs skip: how the reading is taken. A durometer drifts downward in the first seconds as the material relaxes, so an instantaneous reading and a 15-second delayed reading on the same part can differ by several points. State which one you want, keep specimens at least 6 mm thick (thin parts read falsely hard because the anvil pushes back), and never stack thin sheets to fake thickness — the air gaps skew the result.
What Changes When Hardness Goes Up
Hardness does not move on its own. Push it up and other properties move with it, mostly against you. This is the part buyers underestimate: they treat durometer as a free choice instead of the entry point to a chain of compromises.
| Property | Direction as hardness rises | Production consequence |
|---|---|---|
| Elongation at break | Drops (often 600%+ at 30A to under 300% at 70A) | Less stretch for snap-fit, deep-draw, or bellows parts |
| Tear strength | Generally falls past the mid-range | Thin walls and sharp corners tear during demold |
| Sealing on rough or uneven faces | Worse | Needs higher clamp load or a flatter mating surface |
| Abrasion resistance and rigidity | Better | Holds shape under load and wear |
| Demolding of thin or soft parts | Easier when harder | Very soft (<20A) parts stick and distort on ejection |
The practical reading: there is no “better” end of the scale. A 70A gasket survives extrusion under bolt load but will not conform to a warped flange. A 30A membrane seals a rough surface with light pressure but tears if you design a sharp internal corner. You are choosing which failure mode you can live with.
Recommended Silicone Shore Hardness by Application
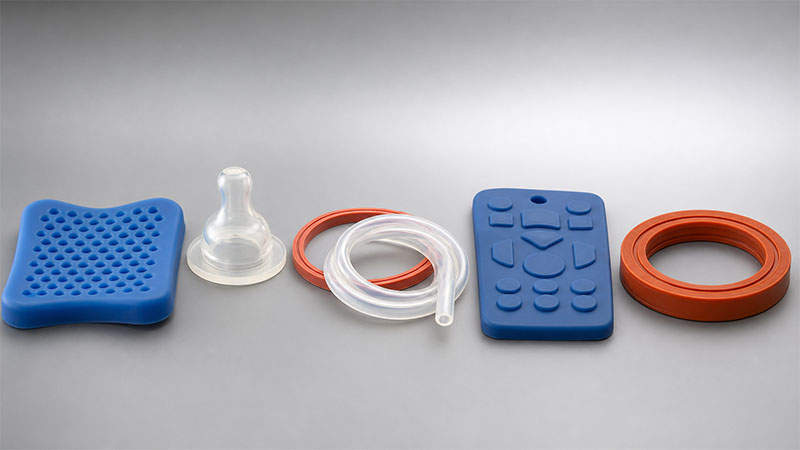
Use these as starting points, then adjust for sealing gap, temperature, and life. They reflect what we actually run, not a textbook range.
| Application | Suggested Shore A | Why |
|---|---|---|
| Anti-vibration pads, soft cushioning | Shore 00 to 10A | Energy absorption matters more than structure |
| Baby nipples, teethers, skin-contact membranes | 20A to 30A | Soft mouthfeel and safe flex; pair with platinum cure and FDA 21 CFR 177.2600 or LFGB |
| General gaskets, kitchenware, soft-touch grips, tubing | 40A to 50A | Balanced flex and recovery; the default for most parts |
| Keypads, handles, structural seals | 60A to 70A | Tactile snap and shape retention under load |
| High-pressure static seals, wear surfaces | 70A to 80A | Resists extrusion and abrasion |
When a part sits between two rows — say a tube that must stay kink-free but also feel soft — do not average. Decide which requirement is non-negotiable and spec to that, then validate the secondary requirement on samples. Averaging two intents produces a durometer that serves neither.
Common Hardness Selection Mistakes
The wrong durometer rarely comes from bad math. It comes from a few predictable judgment gaps.
Treating durometer as comfort. Soft-in-hand and correct-for-function are different questions. A soft grip that needs to resist twist-off needs more durometer than it “feels” like it should.
Specifying a number with no tolerance. ASTM D2240 readings carry real spread. Without a stated tolerance, ±5 Shore A is the working assumption; if your function fails at ±5, the problem is the design margin, not the factory.
Assuming hardness alone defines sealing. Sealing is set by compression set (ASTM D395), gland fill, and surface finish as much as durometer. A correctly chosen hardness in a badly designed groove still leaks.
Reaching for Shore D to mean “durable.” Durable usually means abrasion or compression-set performance, both of which you can tune inside the Shore A range. Jumping to Shore D typically means the part should not be silicone at all.
How Hardness Affects Tooling and Production
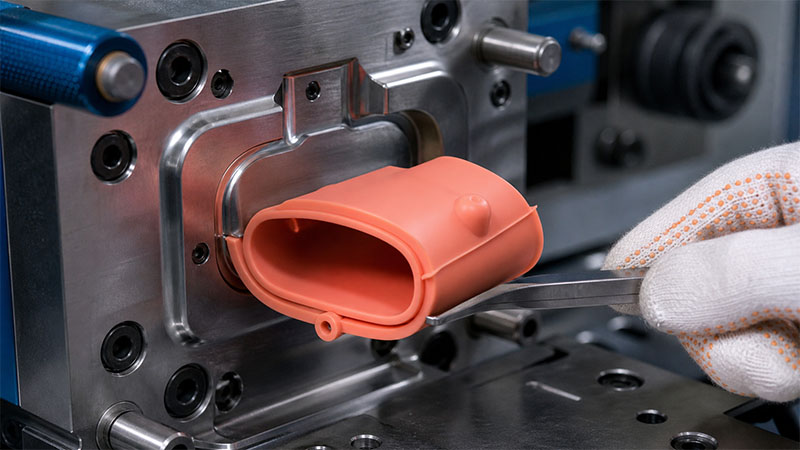
Durometer is set by the compound — base polymer, filler loading, and cure system — before any steel is cut. Raising silica or other filler raises hardness, and up to a point it can raise tear strength too; push filler too high and tear and elongation collapse. That is why “just make it harder” is not a free request.
Two production realities decide cost. First, shrink: a 60A compound and a 40A compound do not shrink identically, so a mold cut for one will hold tolerance on the other only by luck. Change hardness after tooling and you are often re-cutting cavities. Second, post-curing: hardness can drift up a few points after a 200°C post-cure that drives off volatiles, so the number you validate must be the post-cured number, not the green one.
What I Need to Confirm Your Durometer
A hardness call is only as good as the inputs behind it. To lock a number I need: the function and, for seals, the compression gap or target compression percentage; operating temperature range; any regulatory target (FDA 21 CFR 177.2600, LFGB, or USP Class VI / ISO 10993); a hardness tolerance you can live with; surface finish of the mating part; and expected service life. Give me those and I will commit to a durometer and a tolerance. Send a single number with none of them and the risk does not disappear — it just moves downstream to a re-tooling bill once the first run misses.