Most “what is vulcanization” explanations stop at textbook chemistry and never tell you what it changes on the production floor or in your unit cost. That gap is where buyers pick the wrong curing system and pay for it later in odor complaints, tolerance drift, or a failed compliance test.
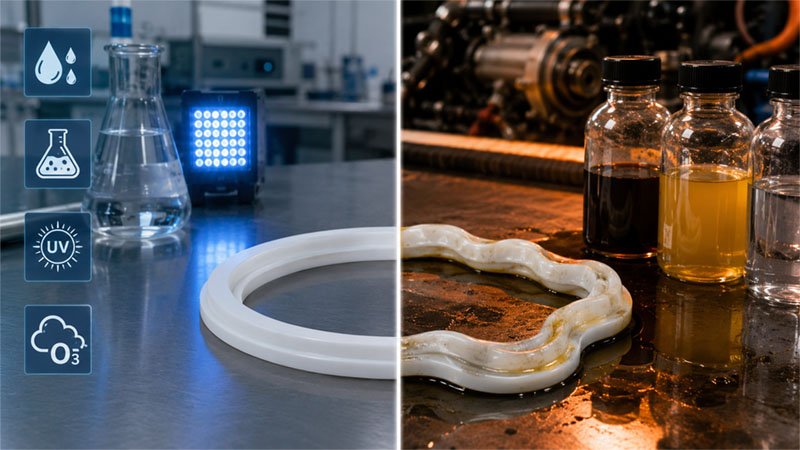
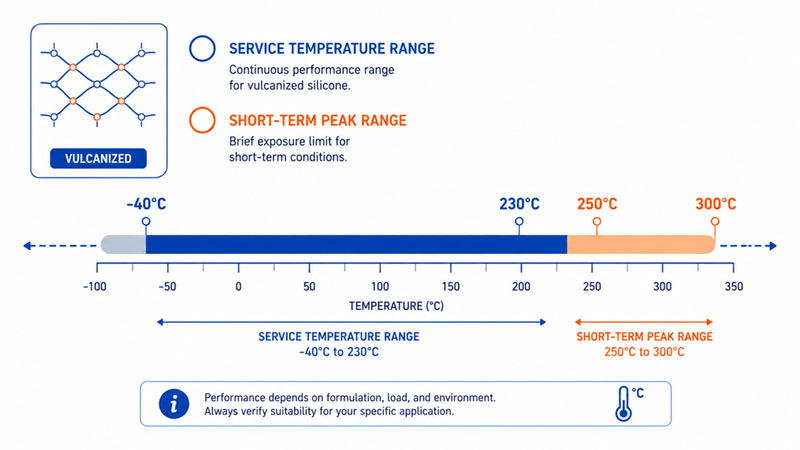
Silicone vulcanization (curing) forms cross-links between silicone polymer chains — triggered by a curing agent plus heat, moisture, or UV/electron beam — turning soft, uncured silicone into a stable elastomer with fixed shape, elasticity, and heat resistance (-40°C to 230°C). The curing system you pick (platinum vs. peroxide) decides odor, food/medical compliance, and cost far more than the base polymer does.
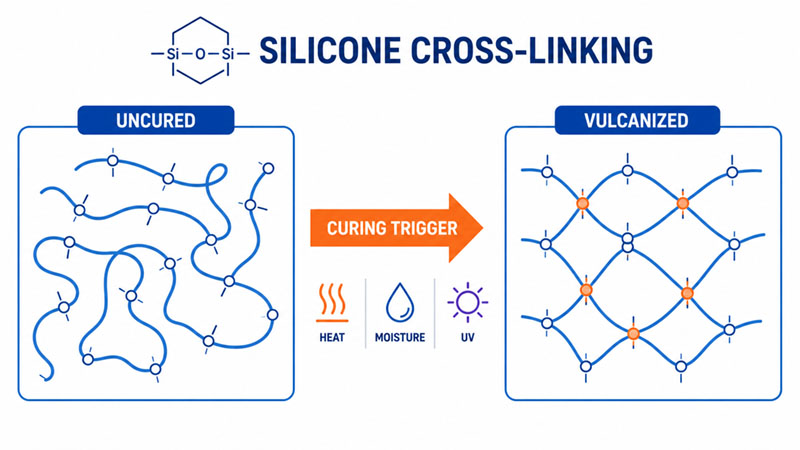
The Three Curing Methods, and When Each Is Used
Vulcanization is defined by how the cross-linking reaction is triggered. Three methods cover almost everything we run:
| Method | Trigger | Typical use | Notes |
|---|---|---|---|
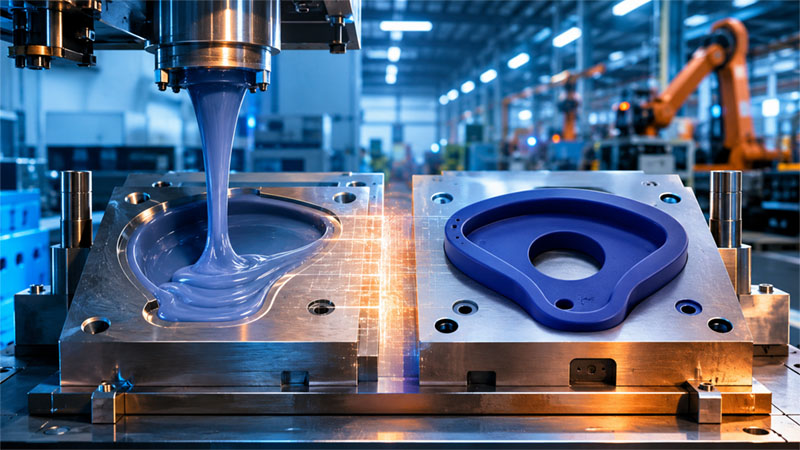
| Heat cure (compression / injection) | Heat + pressure in a mold | HTV molded parts, LSR injection | Highest throughput and precision; needs tooling |
| RTV (room-temperature vulcanizing) | Moisture (1-part) or catalyst mix (2-part) | Sealants, adhesives, low-volume molds | No heated tooling; slower cure |
| Radiation cure | UV or electron beam | Thin coatings, films | Fast, low-heat; limited to thin sections |
For manufactured silicone products, heat-cured HTV and LSR are what we run in volume. RTV is mainly a sealant/adhesive and prototyping route, not a mass-production molding method.
Platinum vs. Peroxide Cure: The Decision That Actually Matters
The base silicone matters less than the curing system. This is the choice that locks odor, compliance, and cost.
| Platinum (addition) cure | Peroxide cure | |
|---|---|---|
| Odor / by-products | None, odorless | Trace odor; needs post-curing to remove |
| Clarity / yellowing | High clarity, low yellowing | Average clarity |
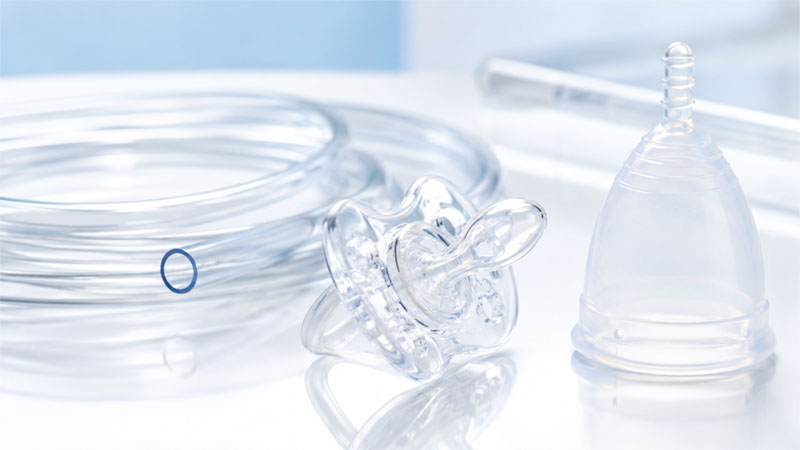
| Compliance fit | Food-contact & medical (pacifiers, tubing, menstrual cups) | Industrial seals, general gaskets |
| Cost | Higher (platinum catalyst) | Lower, best cost-performance |
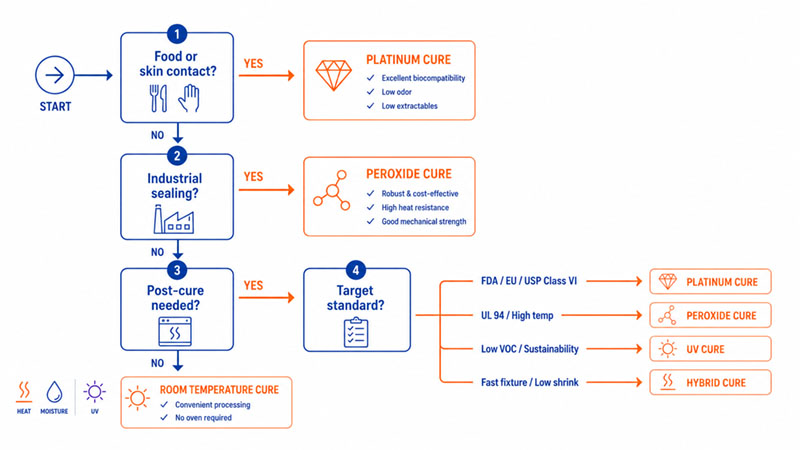
If the part touches food, skin, or the body, it is platinum-cured — there is no shortcut. Peroxide-cured parts headed for sensitive use must go through post-curing (e.g., 200°C for ~4 hours) to drive off residuals, which adds time and cost.
What Silicone Vulcanization Changes About the Material
Cross-linking is what makes silicone usable as a product rather than a paste. In practice it sets:
- Heat range: standard -40°C to 230°C; high-temp grades tolerate short exposure to 250–300°C.
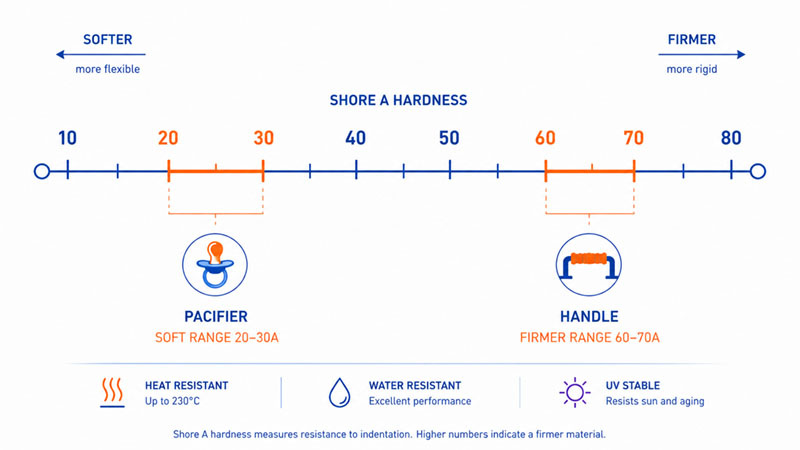
- Hardness: tunable across Shore A 10–80 (≈20–30A for a pacifier, 60–70A for a rigid handle).
- Dimensional stability: cured silicone holds shape and elasticity across its temperature range; uncured material does not.
HTV vs. LSR: Two Ways to Heat-Cure
Both are heat-cured, but the process behaves differently, and that drives MOQ and tolerance.
| HTV (solid, compression) | LSR (liquid, injection) | |
|---|---|---|
| Tolerance | Looser; flash more likely | Tight, down to ±0.02mm |
| Volume fit | Low-to-mid volume | High volume, high cleanliness |
| Tooling | Lower mold cost | Higher mold cost (cold runner) |
| Best for | Simple / larger parts | Medical, baby, precision parts |
Compliance Boundaries to Confirm Before Tooling
The curing system alone doesn’t guarantee a certificate. Match the target standard early:
- FDA 21 CFR 177.2600 — baseline US food-contact.
- LFGB — stricter EU/German food-grade (overall migration testing); material cost typically runs 20–30% higher than plain FDA-grade.
- USP Class VI / ISO 10993 — medical biocompatibility. Note: USP is phasing out the standalone “Class VI” designation (effective Dec 1) in favor of ISO 10993 risk-based biocompatibility assessment, so specify ISO 10993 as the primary reference going forward. Requires production in a Class 100,000 (or cleaner) cleanroom.
FAQs
Is vulcanized silicone food safe?
Only if it’s platinum-cured and certified to the target standard (FDA 21 CFR 177.2600 or LFGB). The cure method, not the label “silicone,” decides it.
Does RTV silicone need heat?
No. RTV cures at room temperature via moisture (1-part) or a mixed catalyst (2-part), which is why it’s used for sealants and low-volume molds.
Why does some silicone smell?
Peroxide-cured silicone can retain trace by-products. Proper post-curing removes the odor; platinum-cured silicone is odorless from the start.
What You Need to Decide Next
Before this becomes a quote, three specs control cost and lead time: target compliance standard (FDA / LFGB / USP Class VI), required hardness (Shore A) and tolerance, and volume/MOQ. Lock those and the curing system, process (HTV vs. LSR), and tooling follow directly.
References
- 21 CFR 177.2600 — Rubber articles intended for repeated use — U.S. eCFR, Office of the Federal Register (current).
- Legal regulations for safe food (LFGB) — German Federal Ministry (BMUKN).
- Use of ISO 10993-1, Biological evaluation of medical devices — U.S. FDA guidance, Sept 2023.
- ISO 10993-1 standard record — ISO catalogue (check current 2025 edition).
- ASTM D2240 — Rubber Property, Durometer (Shore) Hardness — ASTM International.