The silicone vs ABS choice gets treated as a quality contest. It is not. One material is a rigid thermoplastic housing resin. The other is a crosslinked elastomer. If the part must hold a screw, snap, or stay square, ABS is in the conversation. If it must seal, flex, or live through heat and UV, silicone is.
Specify ABS for rigid, impact-loaded parts that stay below the resin’s heat-deflection window. Specify silicone when the part must remain elastic through heat, compression, or outdoor aging. Do not treat LSR overmold onto standard ABS as a default hybrid — the mold temperature is usually above what ABS can hold.
Executive Summary
- ABS is the starting point for rigid housings, bezels, and clips that need impact strength and dimensional stiffness at room temperature.
- Silicone is the starting point for seals, keypad webs, baby/oral-contact flex parts, and any geometry that must recover after repeated deformation or heat.
- Standard ABS is a poor LSR overmold substrate. Typical ASTM D648 HDT sits around 88–100°C at 1.8 MPa, while LSR tools commonly run 120–180°C. Plan an assembled silicone part, or change the plastic.
What Is the Real Difference Between Silicone and ABS?
ABS (acrylonitrile butadiene styrene) is a thermoplastic. It melts, fills a cooled mold, and freezes into a rigid part. That is why it makes housings, covers, and snap features.
Silicone rubber is a thermoset elastomer. After cure it does not remelt. HCR is usually compression or transfer molded. LSR is injection molded into a heated tool. Both silicone routes make elastic parts. Neither route makes a structural shell.
Teams underestimate this because both materials can be “molded.” The machines look similar on a factory tour. The physics are not. ABS carries load in bending. Silicone stores and returns energy. A tensile number on a datasheet does not tell you which function the part has.
For the broader plastic family, use silicone vs plastic. For load-bearing wear parts, use nylon vs silicone. This page stays on ABS.
Silicone vs ABS at a Glance
| Decision factor | ABS | Silicone (HCR / LSR) | Practical verdict |
|---|---|---|---|
| Material class | Rigid thermoplastic | Crosslinked elastomer | Start from the required function, not the resin name |
| Load and stiffness | High; housings, snaps, bezels | Low; designed to deform and recover | ABS for structure |
| Heat under load | ASTM D648 HDT typically ~88–100°C at 1.8 MPa | Many grades stay elastic from about −50°C to 200–250°C | Silicone once heat and flexibility coincide |
| UV / outdoor aging | Yellows and embrittles unless stabilized or painted | Generally stable in UV and ozone | Do not send unstabilized ABS outdoors |
| Food / oral / steam | Possible only inside a defined food-contact authorization | Used for flex food-contact and baby parts when the compound is qualified | Do not swap a nipple or baking surface to ABS |
| LSR overmold | Standard grades warp in a heated silicone tool | Needs a higher-HDT substrate (PC, PA, PBT, metal) | Assemble silicone onto ABS, or change the plastic |
| Scrap route | Thermoplastic regrind possible under control | Cured silicone cannot be remelted | ABS has the simpler scrap path |
The table is a screen, not a specification. Flame-retardant ABS, PC/ABS, and UV-stabilized ABS are different resins. A 30 Shore A LSR seal and a 70 Shore A HCR bumper are equally different.
Which Material Handles Heat Better?
Silicone, when the part must stay elastic after the heat is gone.
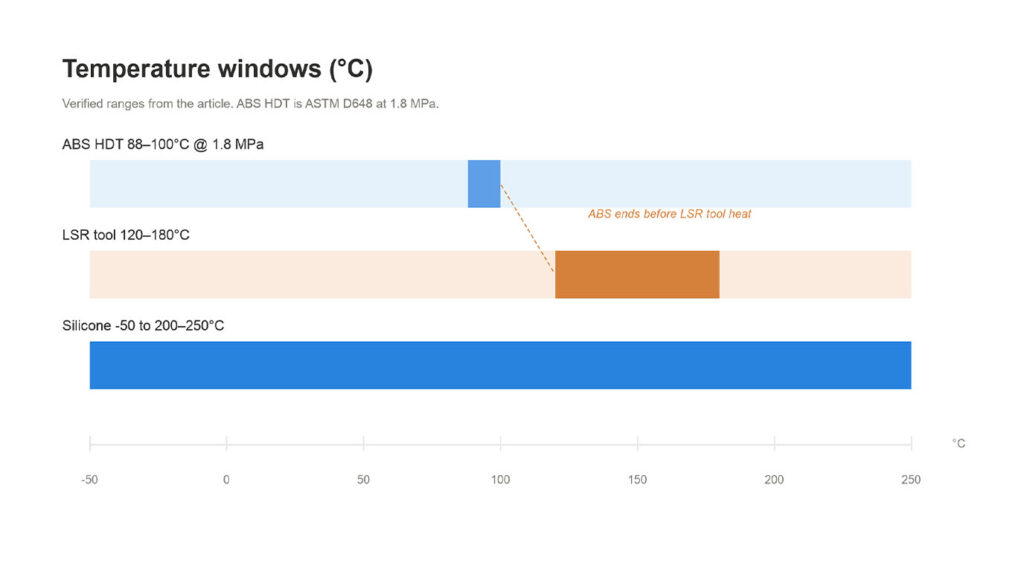
General-purpose silicone grades commonly remain flexible from about −50°C to 200–250°C, grade-dependent. Confirm the limit on the compound TDS. ABS does not work on that curve. Under ASTM D648, unfilled ABS typically deflects around 88–100°C at 1.8 MPa (264 psi), and somewhat higher at 0.45 MPa. HDT is a short-term comparative number. It is not a continuous-use rating, and it is not a license to park the part next to a heater.
The failure we see is later, not on day one. A lid still shuts after a single heat check. After cycling, the seal land has crept, or the cover no longer meets the groove. Teams read “heat resistant ABS” on a brochure and skip the load condition. If service temperature approaches 80°C with load, stop treating ABS as the rigid default.
When Should You Choose ABS?
Choose ABS when rigidity is the product.
It fits:
- Handheld housings and battery covers
- Bezels and cosmetic shells that need a hard, paint-ready surface
- Clips and snaps that must click, not flex
- Indoor parts with impact abuse and no food, skin, or steam duty
ABS is easier to print, plate, and keep glossy than silicone. That matters for a consumer electronics shell. It does not matter for a gasket.
UV is the quiet ABS problem. Unstabilized ABS yellows and embrittles outdoors. Cosmetic housings chalk in months of sun. If the part lives outside, ABS needs a UV package, a paint system, or a different resin. Do not pay for a silicone flex part to solve a UV-housing problem — and do not send raw ABS into that environment either.
When Should You Choose Silicone?
Choose silicone when the part has to move and come back.
It fits:
- Gaskets, valves, and compression seals
- Keypad webs and membranes
- Baking and hot-contact kitchen edges
- Pacifiers, nipples, and other oral-contact flex parts made to a named compliance spec
- Outdoor covers that see UV and ozone
Silicone is not food-contact by polymer name. For repeated US food contact, the rubber listing is FDA 21 CFR 177.2600. EU or German projects add the applicable food-contact framework and BfR Recommendation XV for silicones. Some ABS grades have food-contact authorizations for defined uses. That still does not make ABS a substitute for a 200°C baking surface or a baby nipple.
Related product context: silicone baby products.
Can You Overmold Silicone onto ABS?
Usually not with standard ABS. This is the quoting error that burns tooling money.
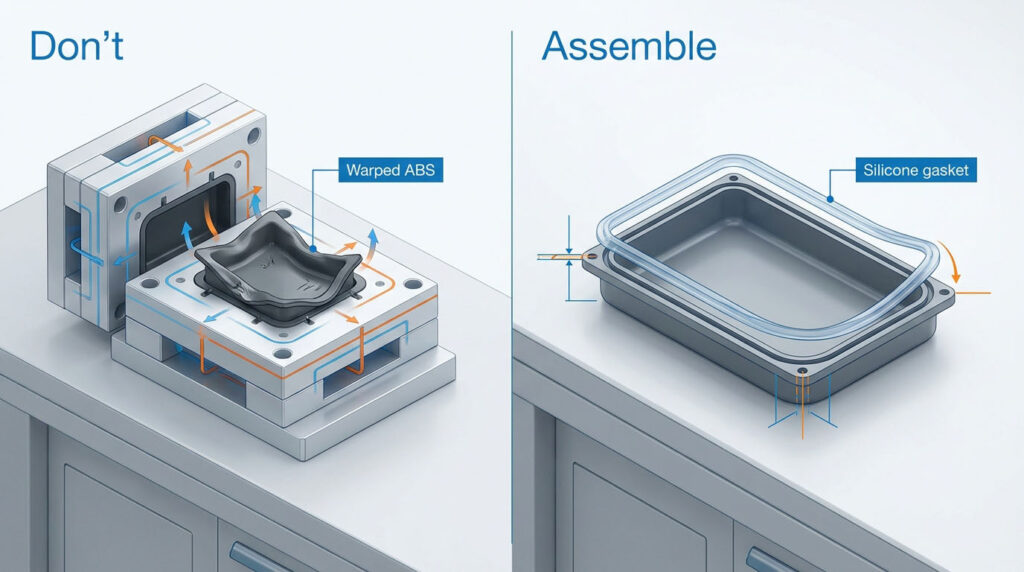
LSR overmolding needs a substrate that survives a heated silicone tool. In our shop, LSR typically cures in-tool around 120–180°C. Standard ABS is already past its HDT there. Published work on medical ABS–LSR molding makes the same point: standard ABS cannot be bonded with silicone in conventional injection overmolding because the heat-deflection temperature is too low. Special ABS grades plus dynamic mold heating show up in research. That is not a production default.
So the hybrid that actually ships is almost never “LSR chemically bonded onto ABS.” It is:
- An ABS housing with a separately molded silicone gasket, keypad, or seal, retained by compression, groove, or fastener
- Or a substrate change to PC, PA, PBT, or metal if true silicone overmolding adhesion is required
If the drawing says “ABS + overmolded silicone” with no substrate HDT check, stop before the mold is cut. Bonding process windows for PC, PA, and metal belong on the adhesion page, not here.
How Do Tooling and Unit Cost Compare?
Do not compare kilogram price.
ABS injection uses a cooled tool, short cycles, and thermoplastic regrind on controlled scrap. Silicone uses a heated tool, cure-limited cycles, and thermoset scrap that cannot be remelted. Deflash is common. Post-cure shows up when a food or medical extraction spec requires it.
ABS usually wins when the part is rigid, volume is high, and the environment is mild. Silicone wins when replacing the part later costs more than the resin — seal failure, heat warp, UV cracking, or a compliance miss.
Volume does not flip the function. A 200,000/year gasket is still a gasket. Molding it in ABS does not create elasticity.
What Do We Need Before Specifying Silicone vs ABS?
Send the function, not the material name:
- Does the part carry load, or does it seal and flex?
- Continuous and peak temperature, including cycling
- Indoor vs outdoor UV
- Food, skin, or sterilization contact, and the destination market (US / EU)
- Annual volume, and whether a two-piece assembly is acceptable
- If overmold is requested: substrate grade and measured HDT, not just “ABS”
If those are missing, any silicone vs ABS recommendation is a guess. We will not guess a tool around it.
For the rest of the material map, start at silicone vs other materials.